



High scrap rates and sluggish assembly lines often trace back to a single component: an incorrect adhesive tape. When a joint fails, production managers frequently blame operator error or substrate variation. Yet, in many cases, the tape itself simply lacks the mechanical compliance or chemical bite required for the job.
Standard flatback paper or filmic tapes frequently buckle on curved surfaces. Foam tapes can be too thick, creating unwanted gaps. This is where double sided crepe paper tape proves its worth on the plant floor.
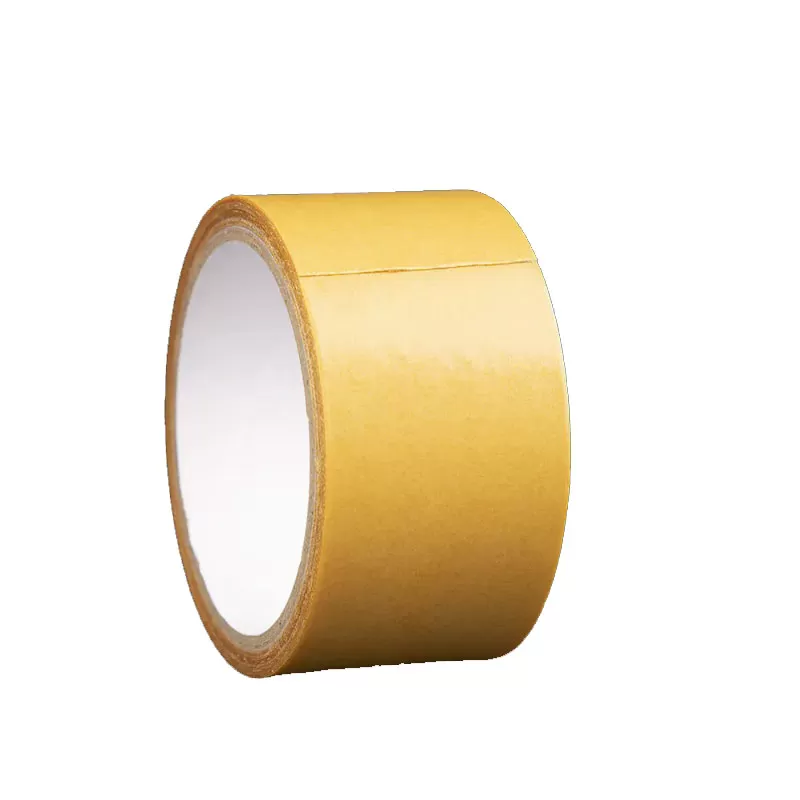
Built with a textured, extensible paper carrier, double sided crepe paper tape combines hand-tearability with exceptional three-dimensional conformability. It fills microscopic surface voids on rough parts while maintaining a low profile. At Youyi, we engineer these tapes to solve the exact bonding, holding, and splicing challenges that off-the-shelf tapes fail to address.
Selecting the right custom crepe tape for manufacturing demands a careful balance of paper weight, adhesive chemistry, liner performance, and converting specifications. This guide walks you through every parameter to ensure your line runs with maximum uptime and minimal waste.
.webp?t=1789717907357 "double sided crepe paper tape")
1. Deconstruct Backing and Adhesive Systems
A tape behaves only as well as its raw components allow. To match your operating environment, you must first evaluate how the crepe paper backing and the adhesive system interact under stress.
The Crepe Paper Carrier: Grammage and Elongation
Creping introduces controlled micro-folds into the paper fibers during manufacturing. This structure gives the carrier its two most critical physical traits: elongation and thickness.
Elongation rate: Standard crepe papers offer between 6% and 15% elongation before breaking. High-elongation papers can stretch beyond 20%, allowing the tape to wrap deep contours and compound curves without lifting.
Basis weight (gsm): Lighter papers (40–60 gsm) maintain flexibility for tight corners. Heavier papers (70–100+ gsm) provide the mechanical bulk needed to absorb vibration and resist shear stress on coarse surfaces.
Internal strength: The paper must have high internal delamination resistance. If the paper splits before the adhesive releases, you face line shutdowns during disassembly or rework.
Adhesive Systems: Matching Chemistry to Substrates
The adhesive layer must wet out quickly and create a durable bond with your specific material surface energy. Off-the-shelf tapes typically use general-purpose formulations that fall short under extreme factory conditions.
Natural rubber adhesive: Delivers rapid wet-out and high initial tack (quick stick). It bonds aggressively to low surface energy (LSE) materials like polyethylene, unprimed plastics, open-cell foams, and textured leather. However, natural rubber degrades under direct UV exposure and prolonged high heat.
Modified acrylic adhesive: Offers superior resistance to oxidation, plasticizers, and chemicals. Acrylics build adhesion over time, creating robust bonds on metals, glass, and engineering plastics. When formulated properly, they withstand harsh thermal cycles without drying out.
Differential tack systems: Many modern manufacturing processes require a tape with two distinct adhesive personalities. We coat one side with an aggressive permanent adhesive to lock onto a trim part, while the exposed side uses an easily removable adhesive that peels cleanly from a temporary jig or fixture.
2. Evaluating Manufacturing Process Requirements
A tape might hold two parts together on a benchtop, but can it survive your manufacturing line? Your production environment dictates the technical thresholds your tape must clear.
Temperature Resistance Thresholds
Thermal loads are the primary cause of adhesive failure in industrial operations. You must assess both the peak temperature and the duration of exposure.
General-purpose crepe tapes begin to soften and bleed around 60°C to 80°C. If your process includes powder coat curing, reflow soldering, or automotive thermoforming ovens, you must specify a high-temperature double coated crepe tape. Formulations stabilized with cross-linked polymers withstand continuous operating cycles between 120°C and 160°C without liquefying, blistering, or charring the paper core.
Balancing Shear Resistance and Peel Adhesion
Procurement teams often look only at 180-degree peel adhesion values. This is an oversight. Peel adhesion tells you how hard it is to strip the tape away from an edge, but shear resistance tells you how well the tape resists sliding forces under a constant load.
For applications like carpet positioning, automotive headliners, or vertical trim mounting, static shear is the decisive metric. A heavy duty crepe paper tape supplier will tune the adhesive rheology to offer high cohesive strength, preventing parts from creeping downward over weeks of static tension.
Clean Removal and Residue Control
Not every tape is meant to stay forever. Splicing, temporary positioning, and manufacturing masks require rapid, clean removal. If an operator spends thirty seconds scraping gummy adhesive residue off an expensive component, your labor costs spike.
By balancing cross-linking density in the adhesive matrix, custom double sided crepe paper tape releases cleanly from metals, tooling, and finished plastics without fiber tear or sticky residue.
3. Customization for Automation and Die-Cutting
Converting and automated dispensing require very specific physical tape characteristics. Even the strongest adhesive fails if the tape jams a high-speed applicator or gummed-up rotary die blades.
Release Liner Selection
The release liner protects the adhesive prior to use and dictates how smoothly the tape unwinds on your machinery.
Glassine paper liners: Dense, smooth, and moisture-resistant. Glassine is the industry standard for high-speed automated dispensing and rotary die-cutting because it resists blade strike-through and releases cleanly under high web tension.
Poly-coated kraft (PCK) liners: Coated with polyethylene on one or both sides. PCK resists moisture curl in humid manufacturing plants and offers excellent dimensional stability for flatbed die-cutting.
Film liners (PET/BOPP): Used where zero paper tear can be tolerated during rapid manual or robotic peel cycles.
Precision Die-Cutting and Oozing Prevention
When running die-cut double sided crepe tape through stamping presses, soft adhesives tend to migrate outward—a phenomenon known as adhesive oozing. This leads to edge bleed, rolls fusing into solid blocks on the shelf, and adhesive transfer onto cutting blades (blade bleeding).
Through custom formulating, Youyi balances the viscoelastic profile of the adhesive. By increasing the internal cohesion of the coating, we produce tape stocks that punch cleanly, yield sharp edges, and eject smoothly from intricate male/female dies without web breakage.
Slitting Formats: Rolls, Spools, and Bobbins
Down-time from roll changes reduces production line efficiency. To optimize continuous manufacturing lines, consider the delivery format:
Pancake rolls: Standard single rolls slit to widths from 3mm to over 1000mm. Ideal for batch assembly and manual application.
Spool/traverse wound rolls: Thousands of meters of tape wound across a wide central core. Spools keep continuous extrusion lines and automated splicing units running for entire shifts without roll changes.
4. Industry-Specific Applications
Double sided crepe paper tape bridges the gap between rigid film tapes and costly foam tapes across multiple sectors.
Automotive Interior Assembly
Modern vehicle cabins contain deeply contoured surfaces covered in fabrics, synthetic leather, sound-dampening felts, and low-energy plastics. Double sided crepe paper tape molds into door panel recesses, bonds acoustic pads to dashboard assemblies, and holds wiring harnesses firmly in place before final cladding is secured. Its paper core dampens buzzing and rattling noises (BSR/NVH reduction) better than thin polyester carriers.
Footwear and Leather Goods Fabrication
Shoe factories and luxury goods manufacturers rely heavily on industrial crepe tape for leather splitting, hem folding, and part positioning prior to final stitching. The tape must grab oily or fibrous leather instantly without bleeding through the grain or gumming up sewing needles. Natural rubber formulations are exceptionally suited for these fibrous, flexible substrates.
Paper Mills, Corrugated Board, and High-Speed Printing
Web breaks halt printing presses and corrugating lines, costing thousands of dollars per hour. Using industrial splicing crepe tape allows continuous-motion flying splices. The high tensile strength of the paper carrier absorbs sudden tension shocks, while the immediate wet-out of the adhesive catches the moving web instantly at full operating speeds.
5. Supplier Vetting Checklist for B2B Procurement
When you source a custom industrial tape, you are not buying an off-the-shelf commodity. You are hiring a manufacturing partner. Use this checklist during your supplier audits:
Lab verification: Can the supplier provide comprehensive technical data sheets (TDS), safety data sheets (MSDS), and compliance test reports (RoHS, REACH, VOC/fogging standards)?
Testing protocols: Do they evaluate adhesive performance using standardized PSTC, ASTM, or FINAT test methods for shear, peel, and loop tack?
Custom prototyping agility: What is their minimum order quantity (MOQ) for non-standard widths, differential coatings, and specialized liners? How quickly can they supply slit hand-samples or pilot-run master rolls?
Process control: Look for ISO 9001 certification. Your supplier must prove they control coat-weight consistency across the entire web to eliminate dry spots and edge-lift failures.
Frequently Asked Questions
Q1: Why choose a crepe paper carrier instead of a film (PET/PVC)
carrier for double sided tape?
A1: Crepe paper
offers high elongation and compressibility that rigid film tapes lack. It
compresses and conforms into textured, porous, or irregular surfaces, providing
higher contact area and better initial grab. Additionally, operators can
hand-tear crepe paper tape without scissors, which accelerates manual assembly
steps.
Q2: How does temperature affect the shelf life of double sided crepe
tape?
A2: Most industrial crepe tapes have a shelf
life of 12 months when stored at 20°C (68°F) and 50% relative humidity. Elevated
warehouse temperatures accelerate adhesive aging, especially for natural rubber
adhesives, leading to loss of tack or liner transfer issues. Keep rolls in their
original packaging away from direct sunlight.
Q3: Can double sided crepe paper tape replace liquid adhesives on the
assembly line?
A3: Yes, in many applications.
Pressure-sensitive crepe tape eliminates the drying time, volatile organic
compound (VOC) emissions, uneven thickness, and specialized ventilation
equipment required by liquid solvent adhesives. Parts bond immediately, moving
directly to the next production phase without curing delays.
Q4: How do I avoid "telescoping" rolls when ordering custom slit
tape?
A4: Telescoping (where the center of the roll
pops outward) occurs when winding tension is set incorrectly for flexible,
stretchy carriers like crepe paper. Tell your converter the unwind speed and
feed direction of your machinery so they can adjust slitting and rewind tension
curves specifically for your line.
Q5: What makes a double sided crepe tape suitable for clean
removal?
A5: Clean removal depends on the balance
between cohesive strength (the adhesive holding itself together) and adhesive
strength (the bond to the part). A tape designed for clean removal uses an
adhesive with high internal cross-linking paired with a high-tensile crepe paper
that will not tear or split when pulled at sharp angles.
Optimize Your Production Line with Youyi
Adhesive tape should never be an afterthought in your engineering process. The right custom double sided crepe paper tape eliminates rework, secures challenging components, and keeps high-speed production lines operating smoothly.
As an established double sided crepe paper tape manufacturer, Youyi works directly with your engineering and procurement teams. We formulate the right adhesive chemistry, slit to tight tolerances, and convert tapes precisely to your operational requirements.
Ready to improve your assembly yields? Contact our technical sales department today. Provide your substrate details, operating temperatures, and dimensions to receive a custom engineering evaluation and a free sample kit for line testing.